
A stranding-machine specification sheet contains several numbers that look comparable but describe different things. Bobbin count is a machine configuration. Cage rpm is a rotation rate. Lay length is a product geometry. Line speed is the cable’s forward travel. Reading each number in context prevents a high catalog maximum from becoming an unrealistic production promise.
Bobbin count describes positions, not the finished core count
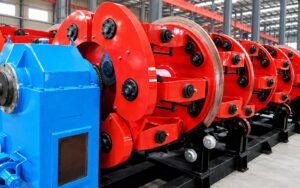
A cage may be offered in 6, 12, 18, or 24-bobbin sections. These numbers describe material supply positions in the specified configuration. They do not automatically state the number of insulated cores in a completed cable, nor do they tell you whether every position is used for a given construction. Drawings and a proposed machine layout are needed to connect the supply positions to the strand arrangement.
When comparing two offers, check the number of cage sections, positions per section, material on each reel, reel dimensions and loaded weights, and the loading method. The same total number of positions can be arranged differently across machines.
Cage RPM is the rotation rate of one machine part
RPM means revolutions per minute. A published maximum cage rpm refers to a particular model and configuration; it is not the cable’s forward speed. For example, BYC’s JLK500 frame-strander table lists maximum cage speeds of 180, 165, 150, and 135 rpm for its 6, 12, 18, and 24-position configurations respectively. This illustrates why a single headline speed cannot describe every version of the machine.
Ask whether the quoted rpm applies with the required reel load, material, guarding, and quality target. A lighter or smaller configuration reaching a higher maximum does not prove that it will produce more acceptable cable per shift.
Lay length defines the helical geometry
Lay length, also called pitch in many stranding contexts, is the axial distance traveled by the product for one turn of a strand around the cable axis. It should come from the cable design or applicable specification. Lay direction and the measurement point also matter. A shorter lay is not automatically better: it changes the helix geometry and may affect material use, flexibility, and downstream handling.
For a simple one-turn-per-revolution process, the unit relationship is line speed (m/min) ≈ cage rpm × lay length (mm) ÷ 1,000. At 100 rpm and a 100 mm lay, the calculated travel is about 10 m/min. This is an illustration of units, not a BYC production rating. Machines with another twist ratio or gearing require the actual transmission relationship, and real operating conditions can impose a lower speed.
Line speed is closer to production travel
Line speed is the length of cable moving through the line per minute. Even when a supplier publishes a maximum line speed, actual output depends on the specified lay, material behavior, tension, reel changes, traction, take-up, and quality checks. Do not multiply a machine’s maximum rpm by its shortest possible lay, or combine several catalog maxima, and present the result as an achievable shift output.

Read the other columns before comparing speed
- Input dimensions: distinguish a single copper or aluminum wire diameter from an insulated core or finished cable diameter.
- Material and reel data: confirm copper, aluminum, or insulated core, along with reel dimensions and loaded weight.
- Pay-off tension: identify the control method and requested operating range for the actual material.
- Traction and take-up: check that the downstream equipment can maintain the proposed line speed and protect the cable surface.
- Tooling and safety: include preforming or compacting, guards, access for reel loading, and the factory layout.
BYC publishes separate frame-strander and 400–800 cage-strander ranges. Compare their model-specific inputs and outputs for the same cable drawing. For the earlier equipment-choice question, see Cage Strander vs. Frame Strander.
A better question for an RFQ
Instead of asking “What is your fastest machine?”, send the conductor or cable drawing, material, single-wire or core diameter, reel size and weight, required lay length and direction, target acceptable output, inspection criteria, and available line layout. Ask the supplier to state a proposed operating speed for that product and explain the assumptions behind it.
Frequently asked questions
Does a 24-bobbin machine make a 24-core cable?
Not by definition. Twenty-four is a machine supply-position count. The finished strand or core arrangement follows the cable design and the way the line is configured.
Can I calculate production speed from cage RPM and lay length?
The simple formula is useful for checking units in a one-turn-per-revolution setup. It does not account for twist ratio, material limitations, tension control, reel changes, or quality requirements. Use the supplier’s validated proposal for planning.
Why can maximum RPM change with bobbin count?
A supplier may list different limits for different cage configurations. Compare the values in the row for the exact model and position count you intend to buy, rather than using the highest number in the table.